Home/Our workshop
From 3 m Bar
to Boxed Fitting
How a handle, leg or bracket is made, finished and checked before it reaches your job.
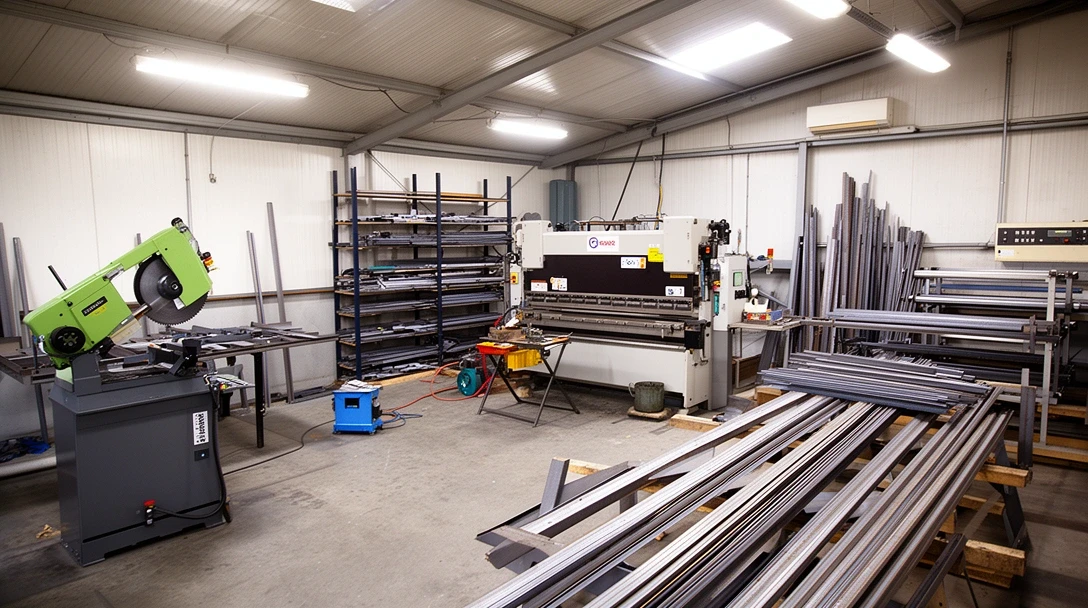
FIVE Stages
The same route for a single knob and a pallet of legs
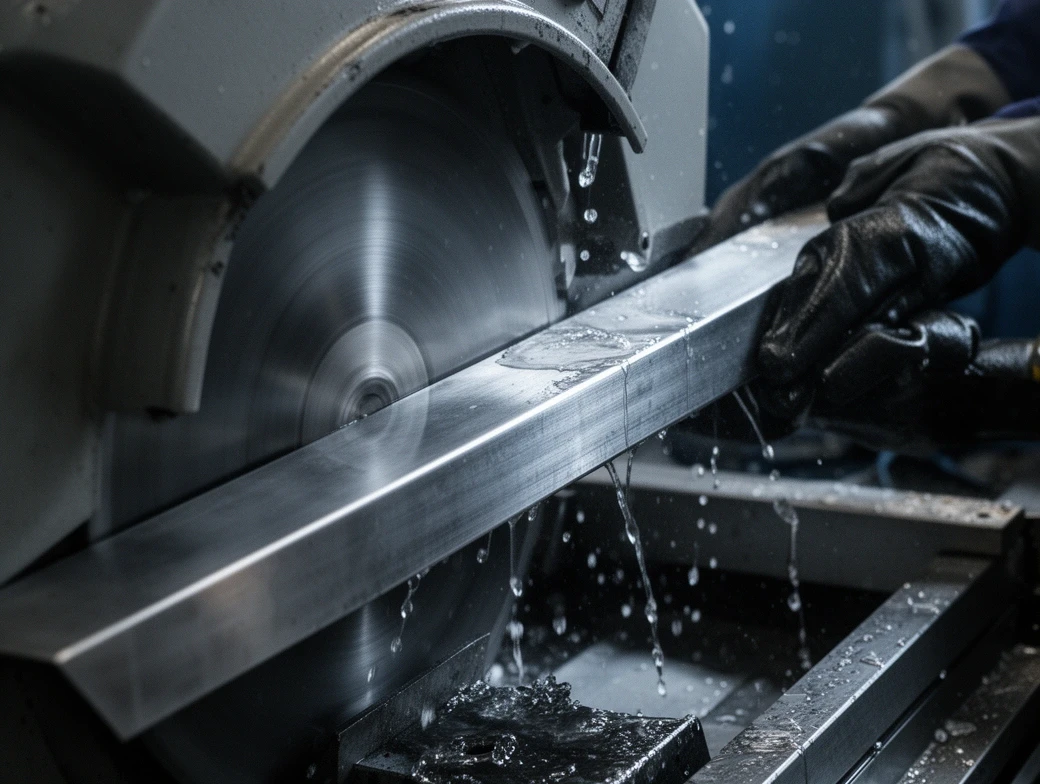
Cutting
Steel, stainless and brass bar arrives in 3 m lengths from UK stockholders. A cold saw cuts each piece to length without heating the metal, so the ends stay square and the finish is not discoloured.
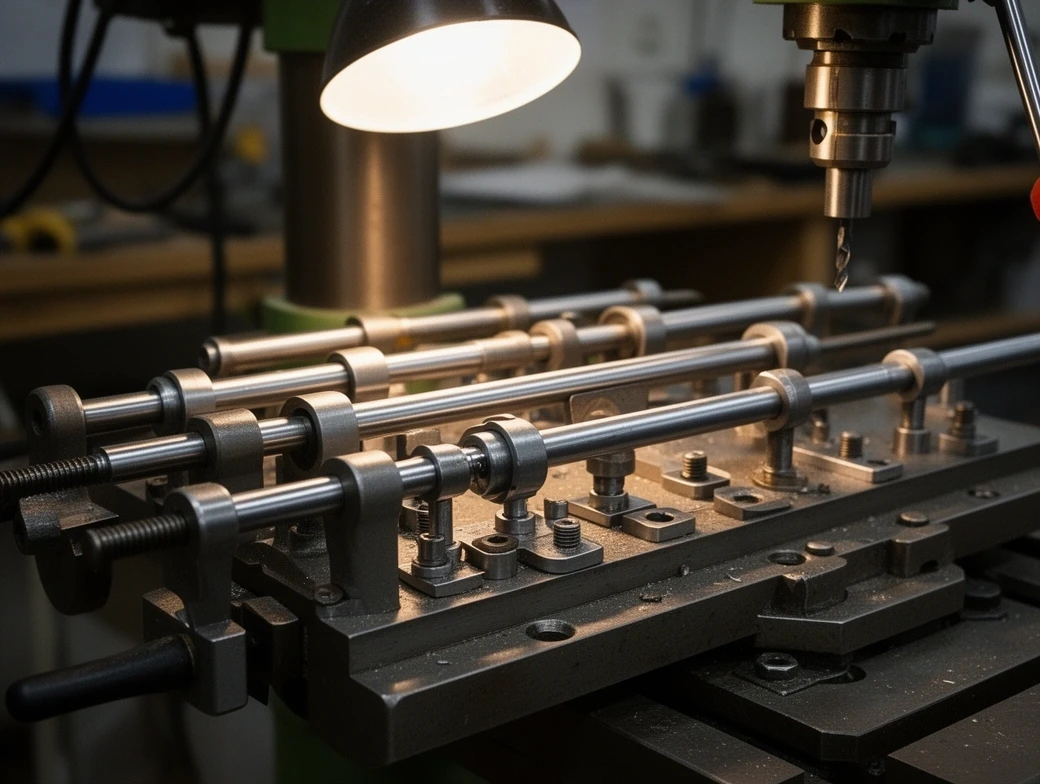
Drilling and tapping
Handles go into a fixed jig that drills and taps both M4 holes in one pass. The jig is what keeps hole centres within 0.2 mm, which is the difference between a handle that fits a pre-drilled door and one that does not.
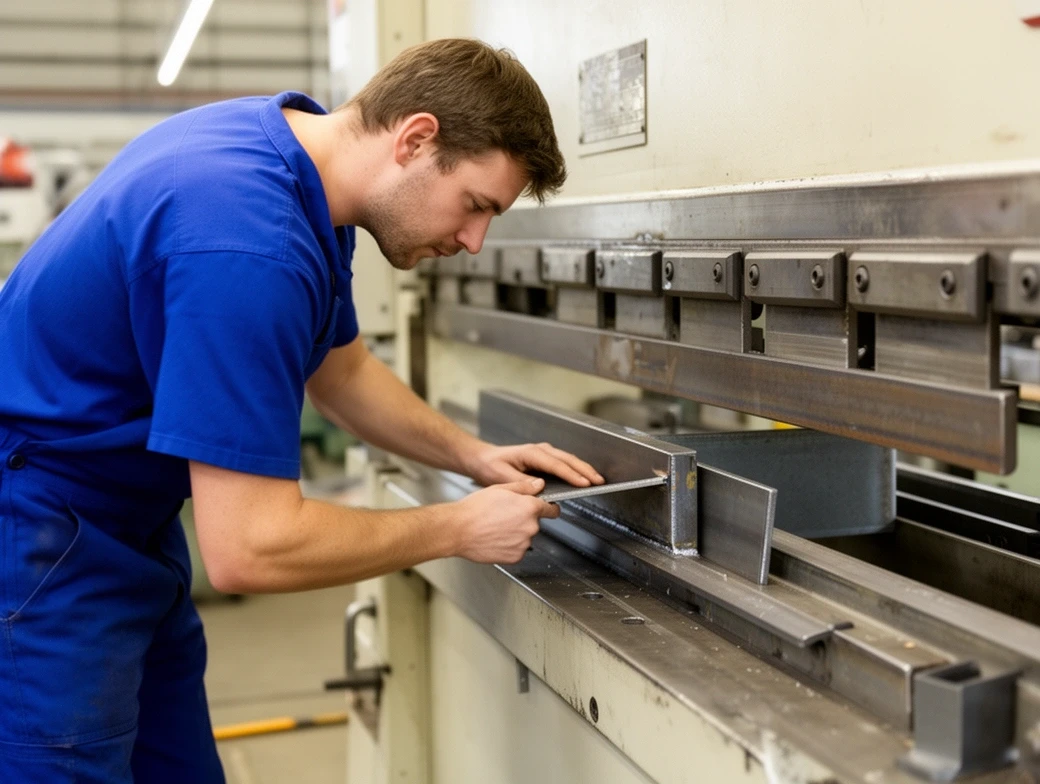
Bending and welding
Brackets are formed on a press brake from 4 mm plate. Hairpin legs and box section legs are welded by hand, then the welds are ground flush so nothing shows through the coating.
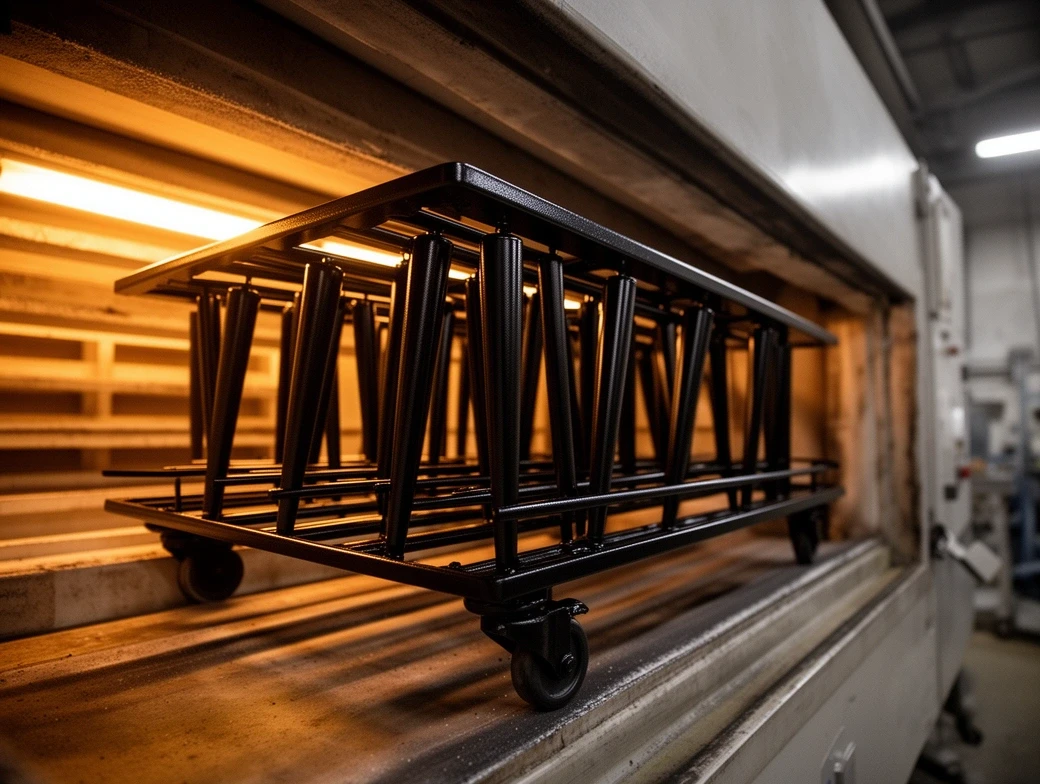
Finishing
Parts are brushed, polished or blackened by hand, or degreased and powder coated in our booth and cured at 180 degrees. Brass is lacquered so it keeps its colour in a kitchen.
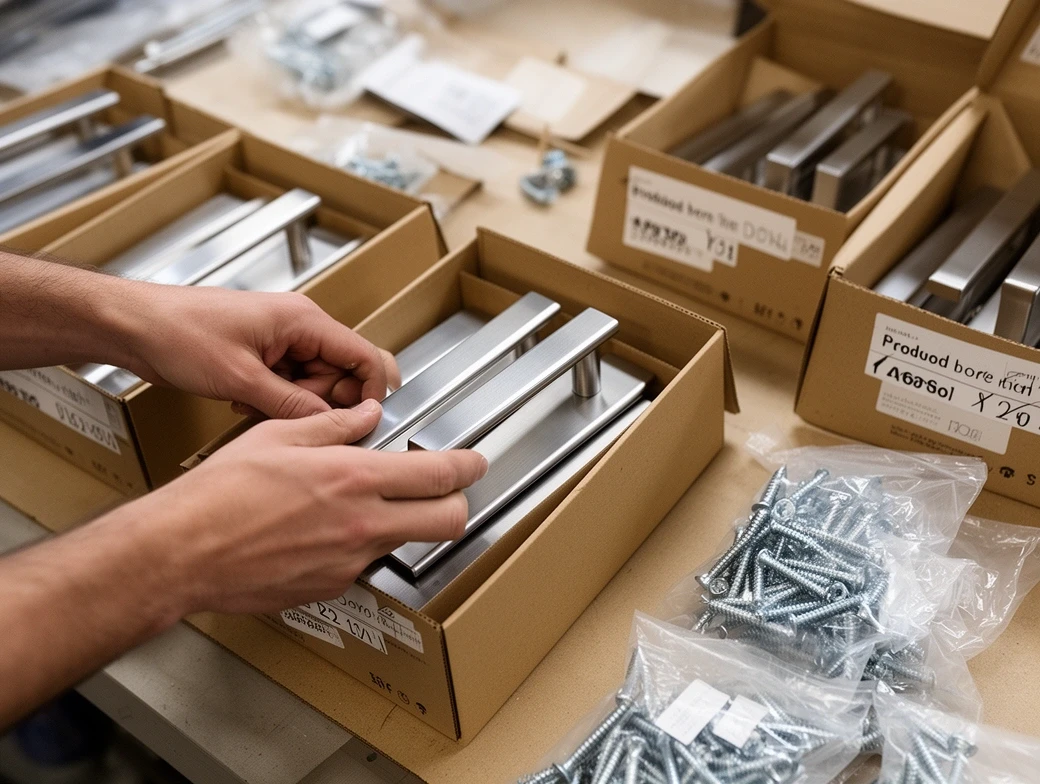
Checking and packing
One part in every 25 is measured with callipers against the drawing. Each box is counted, labelled with the line and batch number, and packed with the right screws.
Materials We Work
Chosen for where the fitting will be used
Legs, brackets and rails. Strong and easy to weld, always powder coated or zinc plated so it does not rust.
Legs · brackets · railsHandles for kitchens and bathrooms. Brushed by hand along the length, it needs no coating and wipes clean.
Handles · hingesKnobs and cup pulls. Turned or cast, then satin finished and lacquered. Heavier in the hand than plated zinc.
Knobs · cup pullsWhat we check before a box is sealed
Every batch gets a card that travels with it through the workshop. If a check fails, the batch stops there, not at your job.
- Hole centres and thread depth against the drawing
- Coating thickness, 60 to 80 microns on legs
- Colour matched to the RAL card under daylight lamp
- Soft close hinges cycled 20 times each
- Welds inspected and ground flush
- Count, screws and label checked at packing